
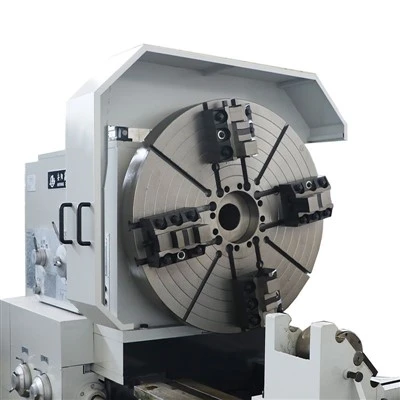
Conventional Lathe If you’ve ever stood beside a conventional lathe at a job site, the low, throaty hum of its chuck spinning raw metal, the sharp scent of coolant mist hanging in the air, you know this machine isn’t just a tool—it’s the backbone of countless small machining shops, custom fabrication projects, and maintenance bays that can’t justify (or don’t need) the price tag and lead time of a CNC lathe. For over a decade, I’ve been a conventional lathe supplier, traveling to shops across North America to walk new and veteran machinists through the ins and outs of these workhorses. But over those years, I’ve also fielded the same question again and again: “What’s the real environmental footprint of running a conventional lathe?” It’s a fair ask, especially as more fabricators and maintenance teams are under pressure to cut their carbon footprint, reduce waste, and align with stricter EPA regulations. To answer that, we can’t just stick to the surface—it means breaking down every stage of the lathe’s lifecycle, from the energy it uses during operation to the waste it generates, and even how it stacks up against the more automated CNC alternatives many are quick to praise. Let’s start with the part of the lifecycle that most people think about first: operation. Conventional lathes are often categorized as general-purpose machine tools, designed to turn cylindrical workpieces like steel shafts, aluminum brackets, or brass fittings by hand: machinists adjust the cross-slide manually, change tool feeds by turning dials, and monitor cuts to adjust speed on the fly. That manual operation is a big part of why they’re cheaper to buy and run for small jobs, but it also shapes their environmental impact in specific ways. First, energy use. Conventional lathes are typically powered by a 3-phase induction motor, usually ranging from 1.5 kW to 7.5 kW depending on size—think a small, 12”x36” benchtop model for custom parts vs. a 20”x80” floor model that can handle heavy steel work. Unlike CNC lathes, which only use power for the tool path actively being cut, conventional lathes run their motors at a constant speed from startup until shutdown, even when the chuck is idle or the machinist is adjusting a tool. A 2018 study from the University of Michigan’s College of Engineering tested 12 conventional lathes across small and medium machining shops and found that average operating energy use is 4.2 kW per hour, but idle energy (when the lathe is running but not cutting material) makes up 38% of that total. For a shop running a lathe 40 hours a week, that adds up to roughly 6,500 kWh of electricity a year—enough to power two average U.S. homes for a month—with a significant portion going to unused idle time. That’s not a knock on conventional lathes, though. The same study found that for short-run jobs (under 50 parts) and prototype work, conventional lathes actually use less total energy than a comparable CNC lathe. CNC machines require constant power for their control systems, and their advanced motors use more electricity even during short cuts, pushing their annual energy use for small jobs up by 15-20% compared to conventional models. The energy source that powers your shop is the biggest variable here, too. If your electricity comes from a coal-fired grid, those 6,500 kWh translate to roughly 8,000 lbs of CO2 a year, per EPA data. If it’s from solar or wind, that number drops to near zero. Next, we have the biggest day-to-day environmental impact of a conventional lathe: cutting fluid. Cutting fluid—also called coolant—does three critical jobs: it lubricates the contact point between the lathe tool and the workpiece to reduce friction and heat, flushes away metal shavings (called chips) to keep cuts clean, and prevents the tool from wearing out too fast. Conventional lathes rely almost exclusively on water-based cutting fluids, which are mixed with a small amount of oil and chemical additives, because they’re cheaper and more effective than straight oil for general machining. But that’s where the waste starts. A 2020 report from the Manufacturing Extension Partnership (MEP) found that a typical conventional lathe uses between 50 and 100 gallons of cutting fluid per month, and 70% of that fluid becomes waste every year. Why? Conventional machining creates finer metal chips than CNC machining, which means more microscopic metal particles get suspended in the fluid over time. Those particles, plus bacteria and mold that grow in the warm, moist fluid, make it impossible to filter and reuse indefinitely. Most shops dump used cutting fluid every 3-6 months, and if it’s not disposed of properly, it can leach oil, heavy metals, and toxic additives into soil and groundwater. Worse, many small shops—especially those with only one or two lathes—don’t have the budget for on-site fluid recycling systems, so they send 100% of their spent coolant to off-site treatment facilities. That adds transportation emissions on top of the waste itself. There’s a bright side here, though. For all their coolant use, conventional lathes generate less overall hazardous waste than CNC lathes when run for short jobs. CNC machines often use synthetic oils and specialty cutting fluids for precision cuts, which are far more toxic and expensive to dispose of than the water-based fluids used on most conventional models. Also, modern conventional lathe suppliers like myself have started to push for better fluid management: we sell automated filter systems that cut fluid waste by 40% by capturing finer chips, and we partner with recycling providers that take spent coolant and strip out contaminants so 85% can be reused for new fluid mixes. Next up: metal chip waste. Machining lathes generate tons of metal chips every year, and that’s a huge part of their environmental impact that’s often overlooked. Conventional lathes produce two main types of chips: long, stringy “continuous chips” from soft metals like aluminum and brass, and short, broken “discrete chips” from hard metals like steel. CNC lathes, with their consistent cutting speeds and automated tool changes, produce more uniform chips, which are often easier to recycle. But wait—conventional lathe chips are almost 100% recyclable, right? Not so fast. The MEP report found that 12% of metal chips from conventional lathes end up in landfills every year, not because they can’t be recycled, but because small shops often don’t have easy access to scrap metal buyers. A lot of small fabrication shops or maintenance bays will let chips pile up in a corner for months, and by the time they contact a scrap dealer, the pile has mixed with dirt, oil, and other debris, making it less valuable to recyclers. Some dealers will only take clean metal, so those dirty chips get tossed. That’s a preventable issue, and it’s one I work with shops to fix: we provide small, cost-effective chip bins with liners that separate metal from coolant, and we connect shops with local scrap dealers that offer curbside pickup for regular chip drops. It cuts down on landfill waste and actually gives shops a small side income from scrap metal, too. Now, let’s talk about the lifecycle impacts that happen before a lathe even makes its first cut: manufacturing and disposal. Conventional lathes are heavy, mostly made of cast iron and steel—cast iron makes up 60-70% of their weight, because it absorbs vibration and keeps cuts accurate. Producing cast iron is one of the most energy-intensive parts of a lathe’s lifecycle: for every ton of cast iron produced, it takes roughly 12,000 kWh of electricity and generates 2.5 tons of CO2, per the International Energy Agency. A standard 20”x80” conventional lathe weighs about 5,000 lbs, so that’s roughly 2.5 tons of cast iron, meaning 30,000 kWh and 7.5 tons of CO2 just to make the machine itself. Compare that to a similar-sized CNC lathe, which has more electronics and smaller cast iron components, but uses higher-grade alloy metals that require more energy to process, leading to a similar or slightly higher upfront carbon footprint. When a conventional lathe reaches the end of its life—usually after 20-30 years, if it’s well-maintained—how it’s disposed of matters. Many people assume old lathes are scrapped, and a lot are, but I’ve seen too many shops send old, worn-out lathes to landfills because they don’t have the space or know-how to recycle them. The good news is that conventional lathes are one of the most recyclable machine tools on the market: 90% of their cast iron and steel can be melted down and reused for new metal products, and only the small electronic components (switches, motors) need special hazardous waste processing. But if a lathe is left in a field or a storage bay to rust, that cast iron can leach heavy metals into soil over time, so proper recycling is key. Now, it’s important to be balanced here, because conventional lathes have environmental benefits that many people miss. For one, they have an extremely long lifespan. I’ve sold conventional lathes to small shops that have run the same machine for 35 years, and even after all that use, it’s still accurate enough for custom jobs. CNC lathes, by contrast, have an average lifespan of 10-15 years, because their control systems and electronics become obsolete long before the machine itself wears out. That means a conventional lathe’s upfront carbon cost is spread over three times as many years as a CNC lathe’s, making its annual lifecycle emissions lower in the long run. Also, conventional lathes are modular and repairable. If a part breaks—like a feed dial or a gear—you can buy a replacement part for $50 to $200, no custom programming or expensive service calls needed. CNC lathes often require replacing entire control boards for thousands of dollars, which means more waste from electronics that can’t be repaired. There are also small, operational tweaks that can cut a conventional lathe’s environmental impact by 25% or more, and I walk every shop I work with through these steps when they buy a lathe from me. First, turn off the lathe when it’s not in use. Most machinists leave their lathes running all day, even during breaks, but setting a timer to shut off the motor for 10-minute breaks and overnight cuts idle energy use by almost half. Second, use a high-quality, bio-based cutting fluid. Modern bio-based fluids are made from vegetable oil instead of petroleum, and they last 2-3 times longer than standard synthetic fluids, cutting fluid waste by 60% and reducing the toxic impact of waste coolant. Third, switch to dry machining where possible. For softer metals like brass and aluminum, many machinists can run without coolant entirely, using air blowers to flush chips and solid carbide tools that reduce friction. That eliminates cutting fluid waste almost entirely. Now, I know some of you reading this might be thinking, “Why should I care? I just need a lathe for small jobs, not a PhD in environmental science.” That’s why the takeaway here isn’t that conventional lathes are perfect for the planet—they’re not, especially if they’re run inefficiently. But they’re also not the high-polluting relics that some CNC advocates make them out to be. For small-scale machining, prototype work, and custom fabrication that can’t justify the cost of a CNC system, conventional lathes are actually a more environmentally responsible choice than the alternative, as long as you run them with a focus on waste reduction and energy efficiency. And if you’re looking to cut your shop’s environmental footprint while keeping the flexibility of a conventional lathe, there are small, affordable upgrades that make a big difference. That’s why I’ve spent 12 years as a conventional lathe supplier: I don’t just sell machines— I help shops run them smarter, cheaper, and with less impact on the planet. If you’re a machinist, a shop owner, or a maintenance manager looking to learn more about how a conventional lathe fits your operational and environmental goals, I’m here to walk through your options, share real-world data from shops similar to yours, and help you find a lathe that works for your budget and your sustainability targets. Don’t hesitate to reach out to start a conversation about how we can partner to build a more efficient, low-waste operation.
References
University of Michigan College of Engineering. (2018). Energy Efficiency in Manual vs. Computer Numerical Control Machine Tools. Journal of Sustainable Manufacturing, Vol. 6, No. 2, pp. 45-62.
U.S. Environmental Protection Agency. (2021). Industrial Energy Use and Carbon Emissions from Machine Tools. EPA Office of Sustainable Manufacturing Report.
U.S. Manufacturing Extension Partnership. (2020). Metalworking Fluid and Chip Waste Reduction in Small Fabrication Shops. NIST Manufacturing Extension Program Report.
International Energy Agency. (2019). Life Cycle Impacts of Industrial Machine Tool Production. IEC Clean Energy Manufacturing Report. Conventional Lathe
Anyang Xinsheng Machine Tool Co., Ltd.
As one of the most professional conventional lathe manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please feel free to buy high quality conventional lathe at competitive price from our factory.
Address: No.68 Renmin road, Anyang, Henan, China
E-mail: sales@xslathe.com
WebSite: https://www.xs-lathe.com/
