If you’re a process engineer, plant manager, or just someone who’s had to troubleshoot valve issues in a high-temp system, you’ve probably stared at a globe valve at 2 a.m. in a boiler room and wondered: Can this thing even handle what I’m throwing at it? As a globe valve supplier who’s been in this game long enough to see parts melt, seize, and surprise folks when they least expect it, let me break this down straight—no textbook jargon, just real-world stuff I’ve witnessed and dealt with. Globe Valve
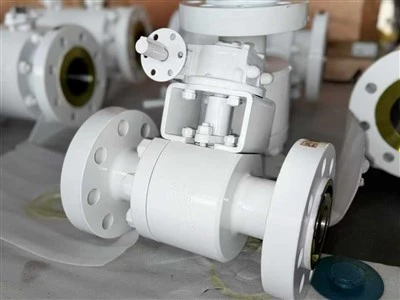
First off, let’s get one myth out of the way right now: I’ve heard so many people say, “Globe valves are for low-temp, low-pressure stuff like plumbing.” That’s such old news, and honestly, it’s why so many people end up grabbing the wrong valve and paying the price. Globe valves are workhorses, and their design makes them actually really good at high-temp applications when you spec them right. Let’s start with the basics of how a globe valve works, because that’s the key to why they hold up (or don’t) in hot environments. Unlike a ball valve that spins 90 degrees to open, a globe valve uses a flat or shaped disk that moves up and down (like a stopper) inside a cage. That means they’re great for flow regulation—not just opening/closing, which is why you see them on steam lines, chemical reactors, and furnace feed lines, all spots where temps can climb way past what a standard valve can handle.
Now, how hot are we even talking here? Because “high temperature” is a loaded term. For most standard globe valves, that’s anywhere from -20°F up to around 450°F, right? But push that limit a little, or go beyond, and you need to adjust the materials. I remember a few years back, a small brewery client came to us panicking because their old brass globe valve on the kettle line blew out when they cranked the steam for a lager batch—temps hit 375°F, which is brass’s upper limit, and the seat started eroding fast. That’s the kind of mistake that’s avoidable if you know what specs to look for.
The sweet spot for globe valves in high-temp applications? It’s actually between 400°F and 1,100°F, which covers tons of industrial uses: power plants, oil refineries, chemical manufacturing, even things like asphalt plants. Wait, can they go higher? Yeah, but you have to get really specific with materials and parts. Let’s talk about the main components that fail in high temps first, because that’s what will make or break this. The body, the disk, the seat, and the stem—those are the four big ones that take the heat. If any of those are cheap or the wrong material, they’re gonna warp, corrode, or seize up.
Take the seat, for example. Standard seats are usually soft metal like Buna-N or PTFE, right? Those max out around 450°F, so if you’re going higher than that, you need a metal-seated globe valve. I’ve got a client in a cement plant that runs their kiln feed lines at 950°F, and they switched from a soft-seated valve that lasted 6 months to a metal-seated one we supplied, and now it’s been going strong for 3 years. The metal seats (usually stainless steel, or even stellite for extra tough stuff) don’t melt, they don’t deform, and they keep a tight seal even when things expand in the heat. That’s the big difference most people miss—grabbing a globe valve with a soft seat just because it’s cheaper, then wondering why it leaks all over.
Next, the stem. The stem is the rod that lifts and lowers the disk, and in high temps, it expands. If the stem expands too much, it can bind in the packing (that’s the seal around the stem to stop leaks). That’s a pain—one client had a valve on a superheated steam line seize up so bad they had to shut down a whole unit on a Saturday, costing them tens of thousands. The fix here is using a stem made of material that has low thermal expansion, like alloy steel or even Inconel for extra hot stuff. We’ve started including that as a standard spec for all our high-temp globe valves, and I haven’t had a call about stem seizing in over a year.
Don’t forget the packing, either. Packing is the set of rings that seals the stem, and in high temps, regular graphite packing can break down if it’s not the right type. Some packings are treated for up to 1,200°F, and if you skimp here, you get leaks—steam leaks are bad, chemical leaks are worse. I always tell clients: if you’re working above 500°F, don’t even look at generic packing. Get the high-temp grade, it’s worth the extra $20 up front instead of $2,000 in downtime.
Now, what about when temps go super high—like over 1,100°F? Can globe valves even handle that? I won’t lie, that’s a stretch, but it’s doable for short periods or specific applications. We’ve supplied some special alloy globe valves for a nuclear test facility that runs at 1,500°F, but those are custom, cost way more, and they’re used more for control than continuous service. For most businesses, you don’t need that—90% of the high-temp jobs I see are between 500°F and 1,000°F, and a properly spec’d standard metal-seated globe valve will hold up great.
Wait, but what about pressure? Because high temp often goes hand in hand with high pressure, right? Steam lines are a perfect example—you’ve got 600°F steam at 1,000 PSI, and you need a valve that can handle both. Globe valves actually do really well here because their design creates a tight seal when pressure increases—unlike some other valve types that start leaking when pressure goes up. That’s why power plants swear by globe valves for their main steam lines. I’ve installed a few myself (well, supervised, I’m not crawling around piping all day, let’s be real) and they don’t budge even when the pressure spikes during a startup or shutdown.
But here’s the catch: it’s not just the material, it’s the installation too. I see so many guys grab a globe valve, stick it in the line, and not account for thermal expansion. When metal gets hot, it expands, and if the valve is installed with too tight of fittings or no expansion joints nearby, it can crack the valve body. Last year, a refinery client had a valve crack because they didn’t leave enough room for expansion on their 800°F line. We fixed it by adding a small expansion spool and tightening the bolts to a specific torque, and that problem never came back. Installation is 50% of the battle when it comes to high-temp valves.
Another thing: valve size. I know it’s tempting to grab the biggest valve you can find for a line that’s carrying hot fluid, but oversized globe valves can cause flow turbulence, which leads to more wear and tear, especially at high temps. Turbulence makes the disk and seat bounce, which erodes them faster. We always help clients size their valves correctly—sometimes that means going smaller than they thought, and they end up with a valve that lasts way longer and works better for flow control.
Let me share a couple of real horror stories and wins to drive this home. A win first: a food manufacturing client that makes pet food, runs their extruder line at 750°F. They were using a gate valve, which kept leaking and couldn’t regulate flow well, so they switched to our metal-seated globe valve. It’s been going strong for 4 years, no leaks, perfect flow control for their extruder. Now the horror story: a construction company that was using a cheap brass globe valve for their asphalt transfer line at 850°F. The valve seized, so they tried to force the stem, which snapped the disk, and asphalt got into the valve body. They had to cut the pipe out, replace the whole valve, and the line was down for 2 days, costing them $50k in delayed deliveries. They came to us, and now we supply them with alloy globe valves for all their high-temp lines—lesson learned, right?
So let’s circle back to the original question: Can a globe valve be used for high-temperature applications? The answer is a resounding yes, but only if you spec it right. A generic, soft-seated brass globe valve? Absolutely not. But a metal-seated globe valve with the right alloy body, stem, and high-temp packing? That’s a workhorse that will last for years in environments that would destroy cheaper valve types.
I get it, as a supplier, I’m biased, but I’m also a guy who’s spent enough time in industrial plants to know that most valve failures are avoidable, and most of that comes down to spec’ing the wrong part. Globe valves aren’t just for cold water or air—they’re perfect for high-temp applications because of their tight seal, excellent flow regulation, and build quality when you use the right materials.
If you’re working on a high-temp project—whether it’s a new steam line, chemical reactor, or industrial process line—and you’re not sure what valve to use, don’t guess. Don’t grab the first valve you find at the supply store. Reach out to us, we’ve got years of experience matching globe valves to exact high-temp needs, we’ll walk you through the material specs, the installation tips, and make sure you get a valve that won’t let you down when the heat is on. We don’t sell one-size-fits-all valves, we work with you to find the right fit for your temperature range, pressure, and application.

Don’t let a cheap valve lead to downtime, missed deadlines, or costly repairs. Hit us up to chat through your high-temp valve needs, and we’ll make sure you get a globe valve that’s built to handle what you throw at it.
Cryogenic Valve References:
- Process Valve Solutions: Selection and Application of Valves for High-Temperature Service, 2021
- Control Engineering: Globe Valve Design and Performance in Extreme Temperature Environments, 2022
- ASME B16.34: Valves – Flanged, Threaded, and Welded End, Pressure- Temperature Ratings, 2019
- Industrial Valve Magazine: High-Temperature Valve Materials and Compatibility, 2020
Zhejiang Poro Valve Manufacturing Co., Ltd.
With abundant experience, we are one of the most professional globe valve manufacturers and suppliers in China. We warmly welcome you to buy customized globe valve made in China here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: PORO Ind. Park, Oubei Dongou Ind. Zone, Wenzhou, Zhejiang, China
E-mail: poro@cnporo.com
WebSite: https://www.cn-poro.com/
