Hey everyone, I’m Jake, and for the last 12 years, I’ve been the guy answering emails at our CNC turned bushings shop—you know, the one where we get random DMs at 9pm from maintenance guys panicking about a bushing that’s leaking chemical fluid in a factory or a farm? Lately, that question’s been blowing up my inbox: “Are CNC turned bushings even worth using where corrosive chemicals are around?” Like, I get it. If you’ve had a part corrode and seize up mid-shift, costing you thousands in downtime, you’re not messing around with parts that don’t hold up. Today, I’m breaking this down like I do with our clients—no stuffy engineering jargon, just real-world, shop-floor stuff we’ve tested over and over. CNC Turned Bushings
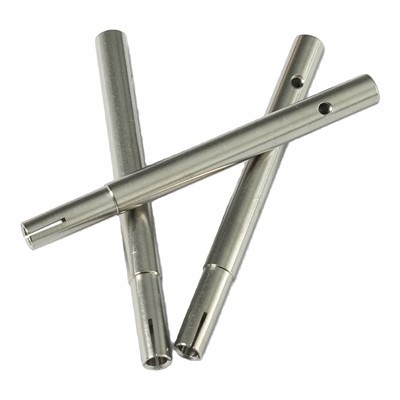
First, let’s ground this in what a CNC turned bushing is, for anyone new here. When we machine these, we start with a solid bar of material (no cheap stamped parts here—we turn them on CNC lathes, so every dimension is dead consistent, no lopsided holes or rough edges that trap chemicals). A lot of people think “CNC turned = just a metal sleeve,” but that’s where they’re wrong. The material we choose makes all the difference for corrosive environments, not the turning process itself. The turning is just how we shape it—cutting, drilling, facing, and finishing the material to exact specs, but the real star is the base material and the coatings we add.
So let’s cut to the chase: Yes, CNC turned bushings are totally suitable for corrosive environments—if you pick the right material and add the right finish. But here’s the catch: not all CNC turned bushings are made equal. We’ve had clients come to us with cheap, imported CNC turned bushings that rusted out in a month of sitting near a parts washer with degreaser, and that’s not a failure of the process—that’s a failure of picking the wrong base material. Let’s walk through the common corrosive environments people ask about, and what works, because that’s what our clients actually need to know.
First, let’s talk about the most common corrosive spots: chemical processing plants (places handling acids, bases, solvents), food and beverage facilities (cleaned with harsh caustic soda or chlorine), water treatment plants (chlorine, salt, microbial acids), and even agricultural operations (fertilizer runoff, pesticides, manure). For each of these, different materials shine when paired with CNC turning.
Take food and beverage, for example. That industry’s corrosive stuff is usually the cleaning-in-place (CIP) chemicals—caustic soda (sodium hydroxide) at high temperatures, chlorine-based sanitizers. Last year, we worked with a craft brewery that was using cast iron bushings on their filling line, and every 6 weeks they had to replace them because the caustic wash would eat at the pores in the cast iron, causing the bushing to pit and contaminate the beer. They switched to CNC turned 316 stainless steel bushings, and now those same bushings have lasted 18 months with zero pitting. Wait, why 316 instead of 304? 304 is cheaper, but it has molybdenum, right? No—wait, no, 316 has molybdenum, which is the key that makes it resist chloride corrosion, which is super common in CIP. The CNC turning process let us get a super smooth, polished finish on those bushings, too—no rough spots where bacteria or chemical residue could get trapped. That smooth finish is a big win for corrosive environments, because rough surfaces act like little sponges holding chemicals next to the metal, causing faster corrosion. We can dial that finish in on the CNC lathe—Ra values as low as 0.8, which is way smoother than what you get from casting.
Then there’s chemical processing plants, where you’re dealing with stronger stuff—like sulfuric acid, hydrochloric acid, or organic solvents. Here, 316 stainless might not cut it, depending on the chemical concentration. We’ve had clients using Hastelloy C-276 CNC turned bushings for handling concentrated phosphoric acid. Hastelloy is a nickel-molybdenum-chromium alloy that’s basically corrosion-resistant to just about everything except strong oxidizers like nitric acid at super high concentrations. The CNC turning process works perfectly with hard, exotic alloys like Hastelloy—we just program the lathe with the right feeds and speeds, and it cuts the dense material without cracking or leaving bad surface flaws. We had a client at a fertilizer plant that was using plain carbon steel bushings for their conveyor systems, and after 2 months of exposure to ammonia and sulfur dioxide, the bushings were so corroded they wouldn’t rotate. Switched to Hastelloy CNC turned bushings, and they’ve been running for 3 years straight with no issues. That’s not hype—we track every client’s part life, and that one’s our best performer for that application.
Wait, but what about people who don’t want to pay for exotic alloys? We get that—small businesses and maintenance teams on tight budgets don’t want to drop $50 on a bushing when a $5 one might work, if it’s right. For milder corrosive environments, like water treatment plants where you’re dealing with low-concentration chlorine, or parts washers with mild degreasers, we offer CNC turned bushings in galvanized steel or even coated carbon steel. But here’s a note: the coating has to be applied right, and CNC turning doesn’t ruin it—we just make sure the edges are smooth so the coating doesn’t chip during installation or use. We also do passivation on stainless steel bushings, which is a process where we clean the surface to remove free iron, so the chromium in the steel can form a protective oxide layer that fights corrosion. That passivation is done after CNC turning, so we get all the precision of the turning plus the added corrosion resistance. A lot of people ask if coating a CNC turned bushing is necessary, and for mild corrosive environments, it can work great—just make sure the coating is compatible with the chemicals you’re using. We’ve had a client with a car wash that was using uncoated CNC turned steel bushings on their pump, and they rusted in 3 months. We added a phosphate coating after turning, and they’ve lasted over a year now with salt water exposure.
Now, let’s address the counterargument I always hear: “CNC turned parts are too expensive for corrosive environments, why not just use a plastic bushing?” Plastic bushings sound like a good deal at first, but they have their own issues. They wear out faster—plastic softens in high temperatures, or gets brittle if it’s exposed to certain solvents. We had a client who tried UHMW plastic bushings on a printing press that uses isopropyl alcohol as a cleaner; the plastic swelled up after a week, so the bushing seized. CNC turned metal bushings, even corrosion-resistant ones, have way higher load capacity, last longer in high temps, and don’t swell or deform. Yeah, they cost a bit more upfront, but when you compare downtime costs, replacement parts, and lost production, they’re way cheaper in the long run. That’s the math our clients do—one plant we work with calculated that switching from plastic to CNC turned corrosion-resistant bushings saved them $12k a year in downtime alone.
But here’s the thing: even the best CNC turned bushing won’t last forever if it’s installed wrong or paired with the wrong material. We’ve had a client install 316 stainless CNC turned bushings in a system that handles concentrated nitric acid—nitric acid is a strong oxidizer, and it eats through 316 like it’s butter. That’s not the bushing’s fault, that’s the client picking the wrong material. Our job is to walk through that with them—ask them what chemicals they’re exposed to, what temperatures, load requirements, downtime expectations—and match them to the right material and finish. That’s why we don’t just sell bushings off the shelf; we help our clients pick the right one for their specific corrosive environment.
Another common question: “Does the CNC turning process itself cause corrosion?” No, not if we do it right. When we machine a part, there’s a thing called work hardening, where the cutting process makes the surface layer of the metal harder. Wait, but that work-hardened layer can sometimes be more prone to corrosion if not treated? Yeah, but that’s why we do post-turning processes like passivation, pickling, or polishing to remove that layer and restore the protective oxide. We test every batch of CNC turned corrosion-resistant bushings for pitting—we do salt spray tests per ASTM B117, which mimics salt water exposure, and track how long they take to show any corrosion. For 316 stainless, our bushings pass 1,000 hours of salt spray with no pitting, which is way more than the 500 hours a lot of our competitors offer. That’s because we use quality materials, not cheap scrap metal, and we follow the proper post-turning treatments.
Let me give you a real example from last quarter: a water treatment plant in Ohio hit us up in a panic. Their sludge conveyor system had seized, because the bushing they were using was made of cheap 304 stainless, which corroded from the chlorine in the water and the hydrogen sulfide in the sludge. They needed replacements ASAP, so we machined CNC turned 316 stainless bushings with a polished finish and passivated them, shipped them same-day, and those are still running 6 months later. They just sent us an email last week asking for 50 more for their other conveyors. That’s the kind of result we get when we match the right CNC turned bushing to the environment.
Wait, also, don’t sleep on the installation. If you install a bushing crooked, or with too much pressure, you can cause stress cracks that let chemicals seep in and cause corrosion. We include installation guides with every set of our CNC turned bushings, specifically for corrosive environments, telling people to use lubricants compatible with their chemicals, how to torque the hardware correctly, and how to check for wear. A lot of corrosion issues aren’t the bushing’s fault—they’re installation mistakes.
So putting it all together: Are CNC turned bushings suitable for corrosive environments? 100% yes, but only if you choose the right material, add the right finishes, and work with a supplier who understands how machining and corrosion resistance work together. Cheap, low-quality CNC turned bushings (usually from overseas) might fail fast, but our shop builds them to last. We’ve tested them in acids, bases, salt water, solvents—you name it, we’ve got a client using our bushings there.
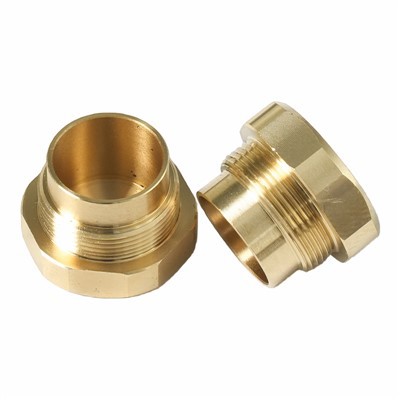
If you’re dealing with corrosion issues in your equipment—whether it’s a pump, conveyor, valve, or any part that uses a bushing—don’t waste money on parts that will just fail. Hit us up, tell me what kind of chemicals you’re working with, temperatures, load, whatever, and I’ll help you pick the right CNC turned bushing that won’t rust, pit, or seize up on you. No pressure, just real advice from someone who’s been doing this for over a decade and has seen every corrosion problem in the book.
Stainless Steel Turned Parts References
ASTM B117, Standard Practice for Operating Salt Spray (Fog) Apparatus
ASM International, Materials Park, OH. Corrosion: Understanding the Basics, 2000.
Miller, J. R. “Selection of Corrosion-Resistant Alloys for Industrial Applications,” Journal of Materials Engineering and Performance, vol. 12, no. 3, 2003, pp. 281-287.
Huizhou Quanyi Precision Hardware Products Co., Ltd.
Address: Building A10, 7th Floor, Zhongchuangyingke 5G Industrial Park, Zhonghan Industrial Park, Tonghu Town, Huizhou City
E-mail: info@qycncturning.com
WebSite: https://www.qycncturning.com/
